
Opening: the core production problem
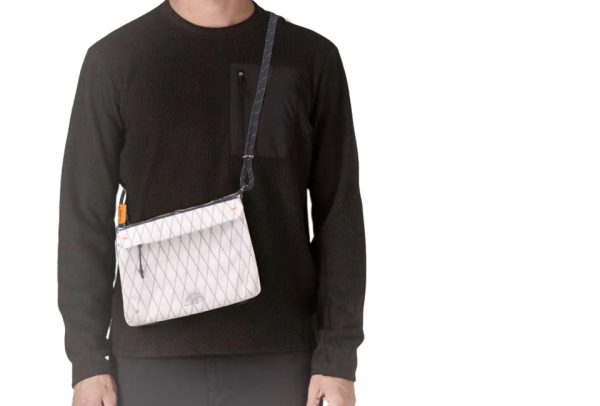
Design teams routinely underestimate the gap between a market-ready concept and a scalable production protocol; when they engage a custom bag manufacturer expecting plug-and-play delivery, misalignment on tolerances, materials, and test criteria creates schedule slips and cost overruns. The immediate problem: lack of reproducible manufacturing inputs — tech packs, material specs, and inspection triggers — that let factories run to plan without repeated sample cycles.
Diagnosing bottlenecks in the factory pipeline
Quantity ramping fails for predictable technical reasons. Material variance (denier, coating thickness), nested-pattern optimization, and hardware lead times (zippers, buckles) create chokepoints. Tooling delays from late die approvals and improper marker layouts increase fabric waste by 5–12% on typical runs. You must quantify each source: measure first-pass yield, time-to-approved-sample, and rework hours per 1,000 units to locate the dominant bottleneck.
Design-to-manufacturing handoff: precise deliverables
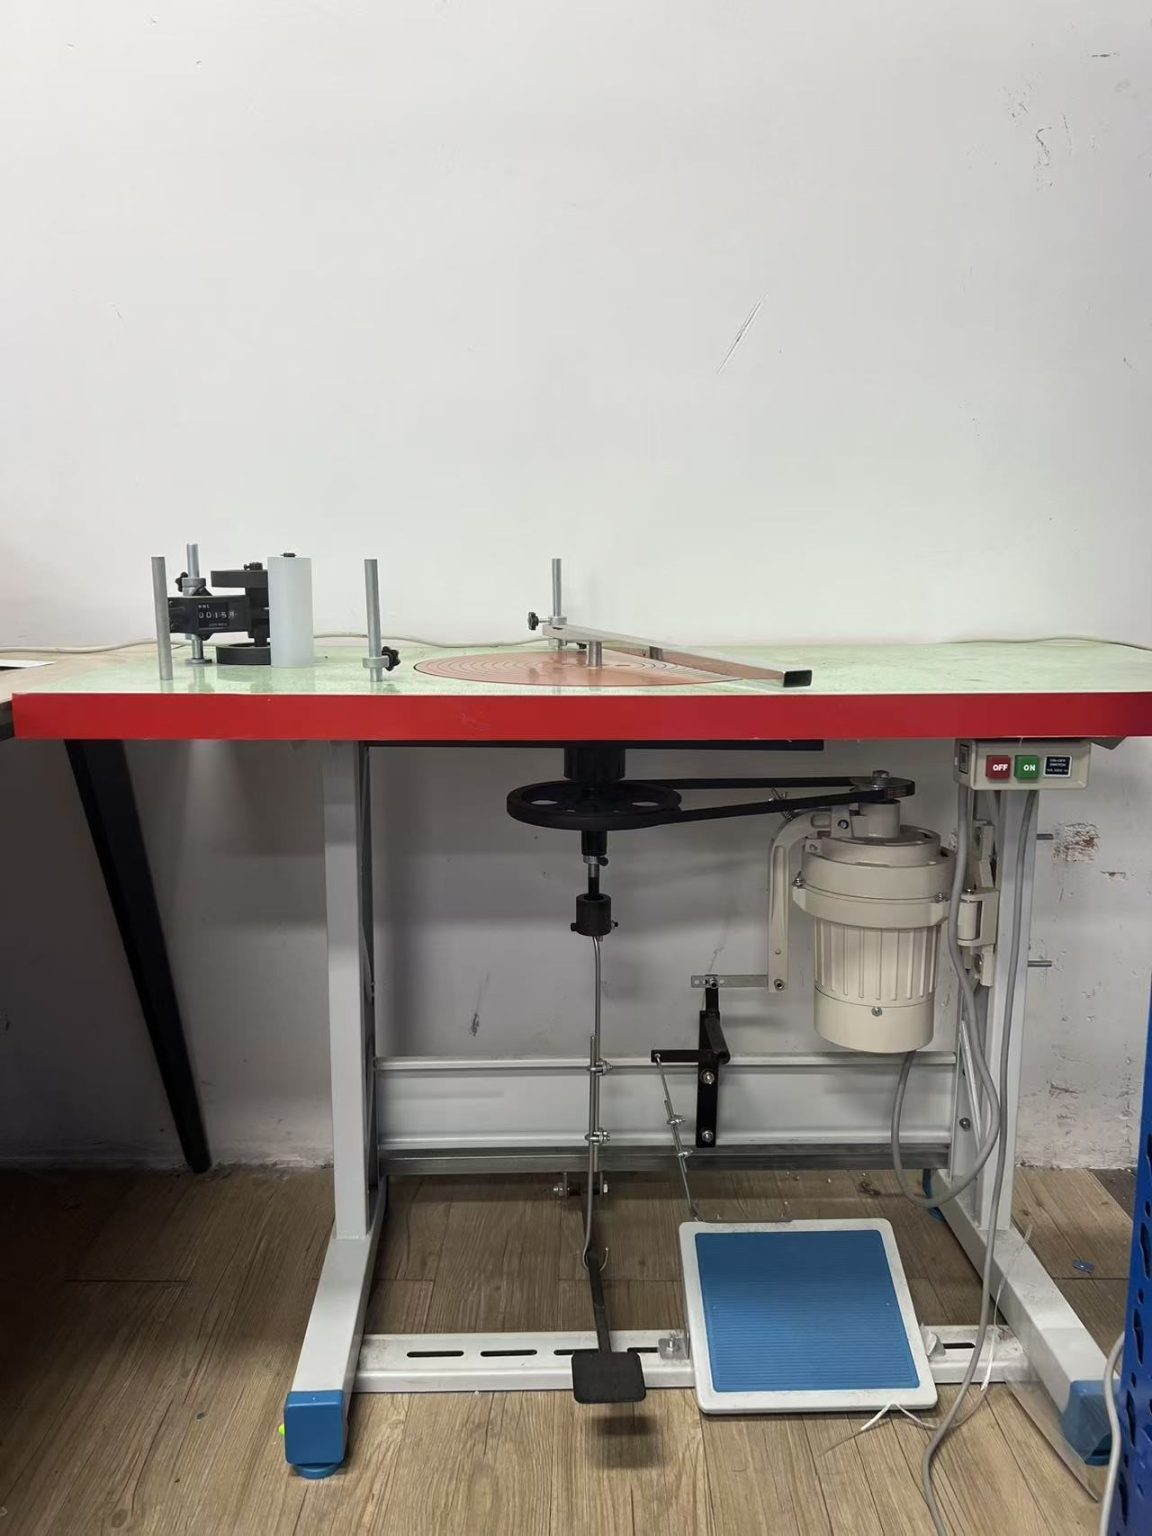
Create a deterministic handoff. Deliverables include a CAD-ready pattern set with annotated seam allowances, graded size table, layer-by-layer construction diagram, Bill of Materials with supplier part numbers, and an inspection checklist with numeric pass/fail thresholds (seam strength in N, zipper pull force in N, water resistance in mm H2O). Avoid vague language; specify stitch type (e.g., 301 lockstitch, 401 safety stitch), thread denier, and hardware plating thickness. CNC-ready DXF files for cutting reduce marker errors and limit material scrap.
Supply selection and sourcing reality (real-world anchor)
Sourcing concentration in Guangdong province — the Pearl River Delta manufacturing cluster — shapes lead times and supplier capability expectations; production flows and component availability there are well documented by trade reports and local show calendars, so many teams consolidate sourcing through a chinese bag supplier that understands local vendor networks and export logistics. That single-location anchor reduces coordination overhead but requires disciplined supplier qualification and export compliance checks.
Quality control: objective tests and inline checks
Implement defined QC gates. Pre-production sample (PPS) with full test report, inline 10% AQL checks per operation stage, and final random tensile and abrasion tests on finished units are minimums. Use quantified thresholds: seam slippage X N/cm, hardware torque tolerance ±Y%. Require raw-material certificates and batch-level traceability for coated fabrics and foam to isolate defects quickly.
Common mistakes and how to avoid them
Teams skip PPFs, accept ambiguous tech packs, or defer hardware sourcing until color approval — each drives rework. Fixes: lock materials before final trim approvals, maintain a library of approved suppliers for fast replacement, and enforce one-source control documents so any change triggers a documented impact analysis. Keep MOQs visible and model cash flow: smaller batches increase per-unit cost but reduce inventory risk; model both scenarios numerically.
Alternatives and trade-offs
Nearshoring reduces lead time but raises per-unit costs by 15–40% and often increases tooling costs. On-demand printing allows SKU diversification but limits structural features (molded foam, complex hardware). Automated cutting and modular assemblies cut labor variance but require capital or third-party service fees. Choose a mix: reserve complex components for established partners and use flexible vendors for seasonal SKUs.
Technical checklist for a production-ready strategy
Checklist items you should enforce: final tech pack with tolerances, validated PP sample with test certificates, approved supplier list and contact matrix, tooling sign-off with lead-time calendar, inline inspection plan with metrics, and post-shipment sampling protocol. Track these items in a simple RACI matrix and measure compliance weekly.
Closing synthesis
Fix the root causes: precise engineering documentation, tight supplier qualification, and measurable QC gates convert concept designs into reliable production runs. For teams that need consistent execution across materials and complex assemblies, a production partner with established local networks and technical depth makes the engineering controls operationally enforceable — a partner such as ChangRong often becomes the standard reference point for sustaining that discipline.